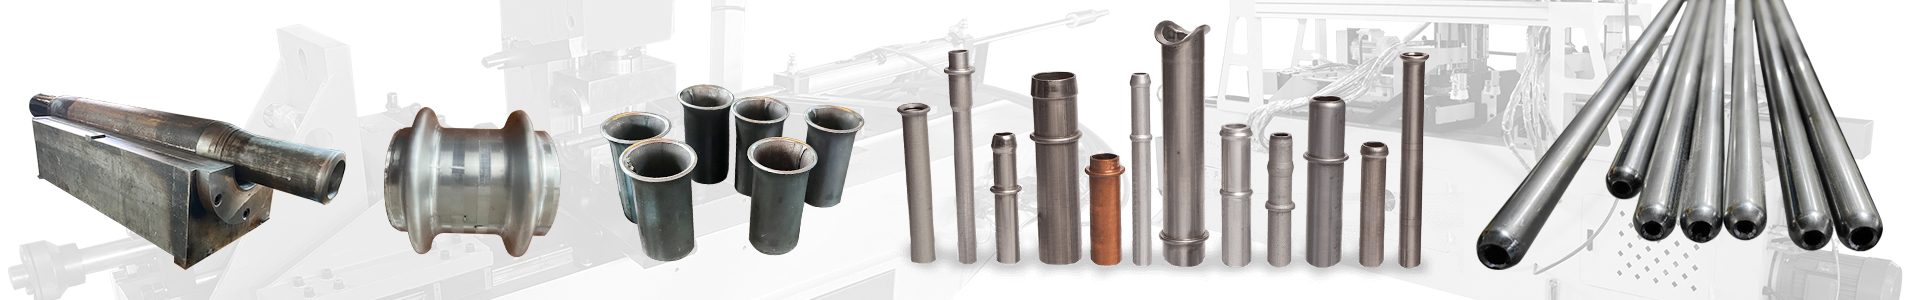
Home / End Forming / Hump Pipe

Item |
Name |
Unit |
Data |
Remark |
|
1 |
Forming cylinder power |
Ton |
20 |
Max 26 ton |
|
2 |
Max forming diameter |
mm |
∅133X2.0 |
Diameter *thickness |
|
3 |
Min forming diameter |
mm |
∅30X2.0 |
|
|
4 |
Min forming length |
mm |
30 |
|
|
5 |
Max forming length |
mm |
No limited |
|
|
6 |
Machine height |
mm |
1150 |
|
|
7 |
Product processing time |
s |
~18 |
Depend on drawings |
|
8 |
Tooling change time |
min |
~10 |
|
|
9 |
Repeated position accuracy |
Outside diameter of hump |
mm |
±0.2 |
Hump forming workpiece tolerance |
|
Hump contour |
mm |
0.2 |
|
||
|
hump thinning |
mm |
≤20% |
|
||
|
|
|
|
||
10 |
Process control type |
Outside diameter of hump |
|
Cylinder +encoder + tooling |
|
|
Hump contour |
|
Cylinder +encoder + tooling |
|
||
hump |
|
Tooling |
|
||
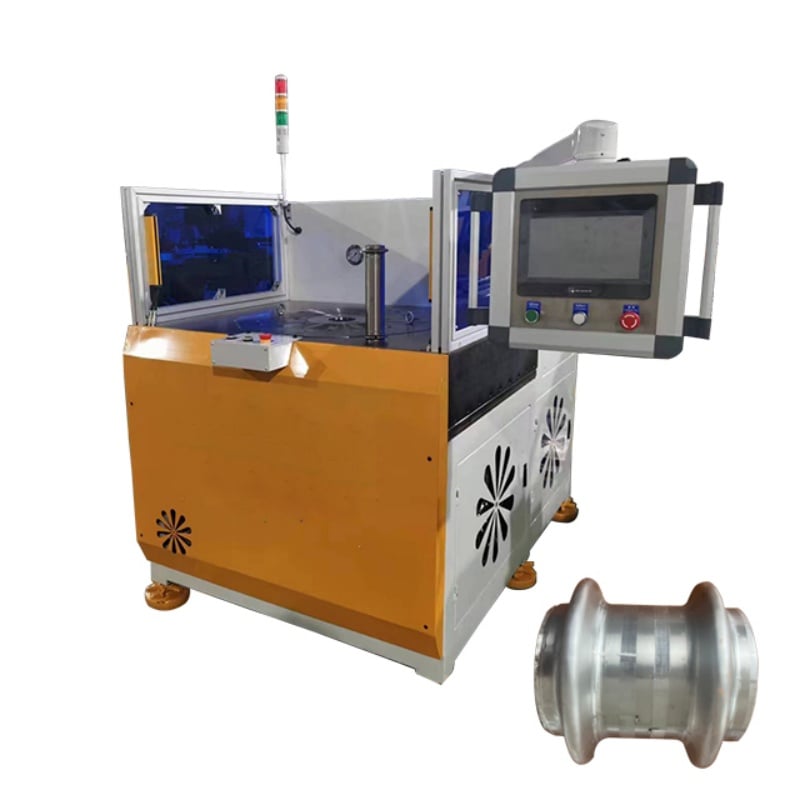
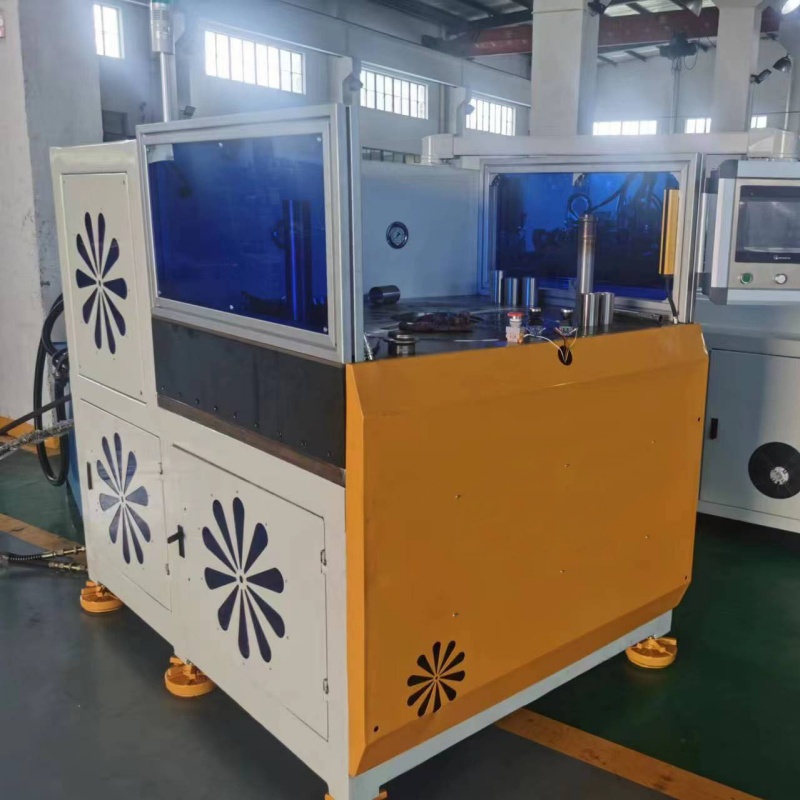
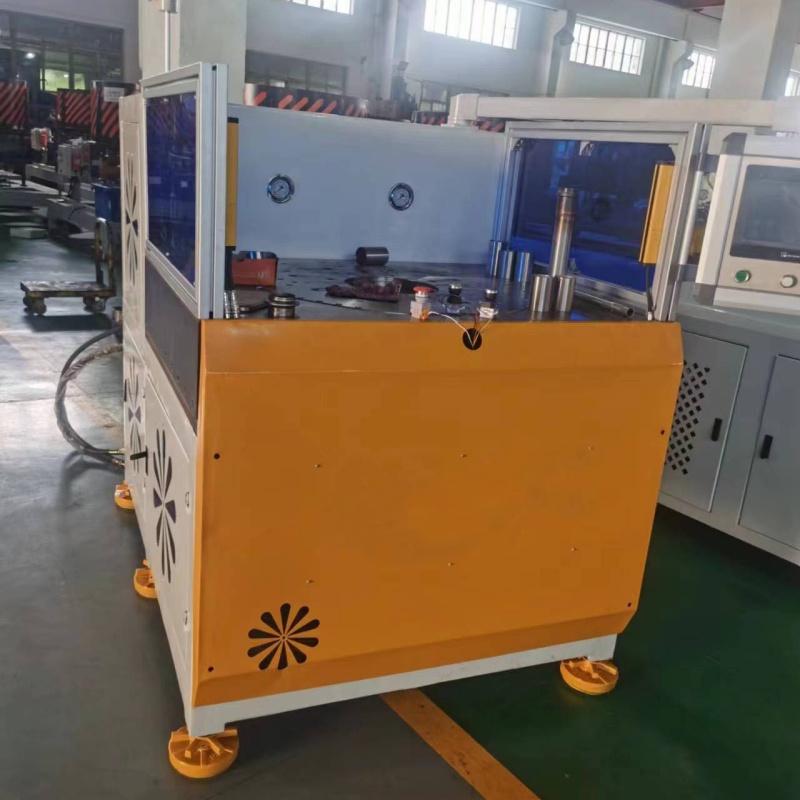
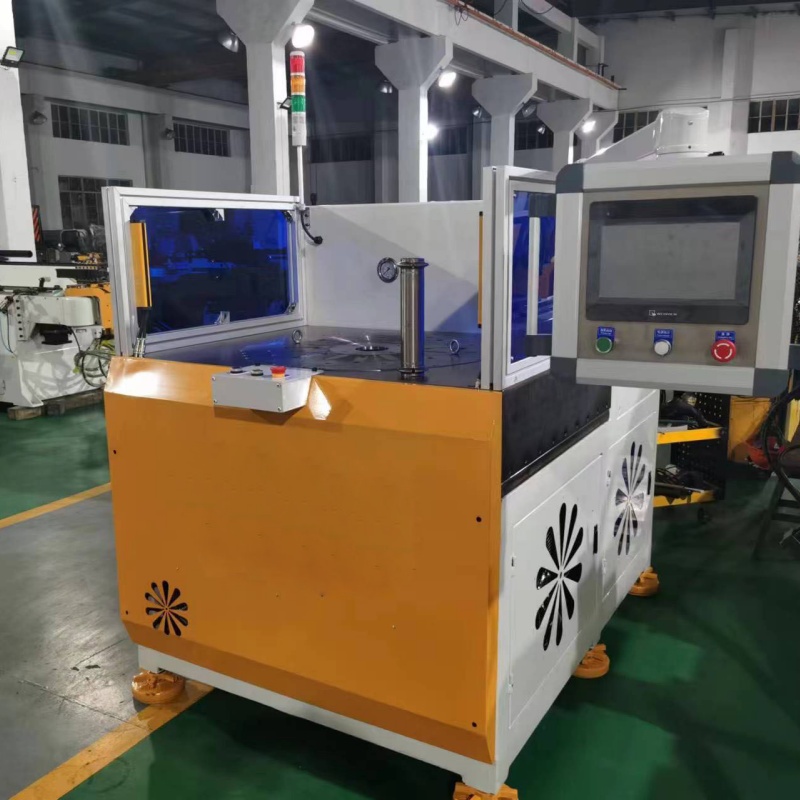
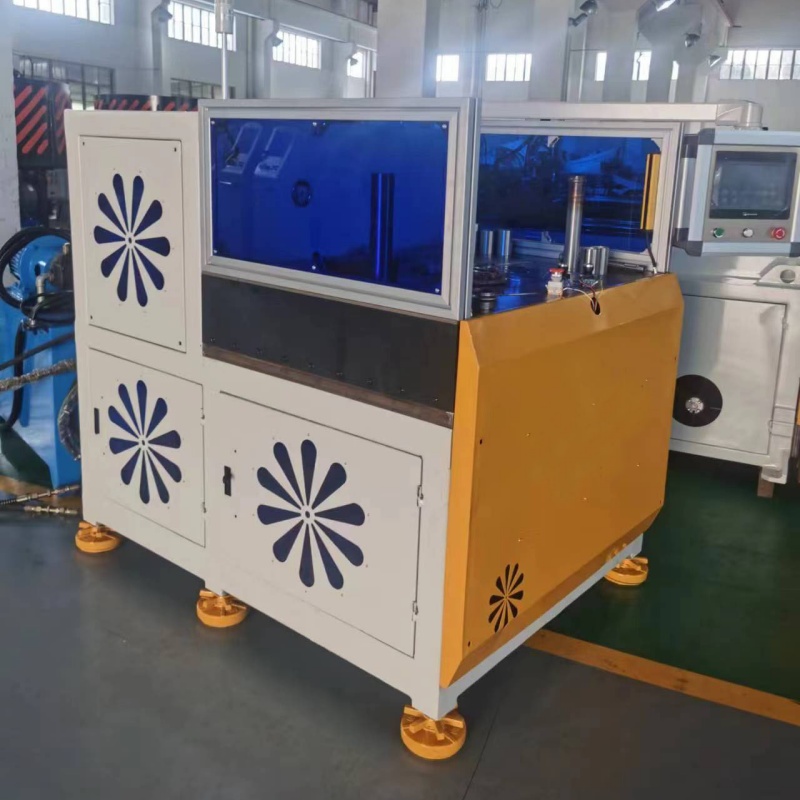
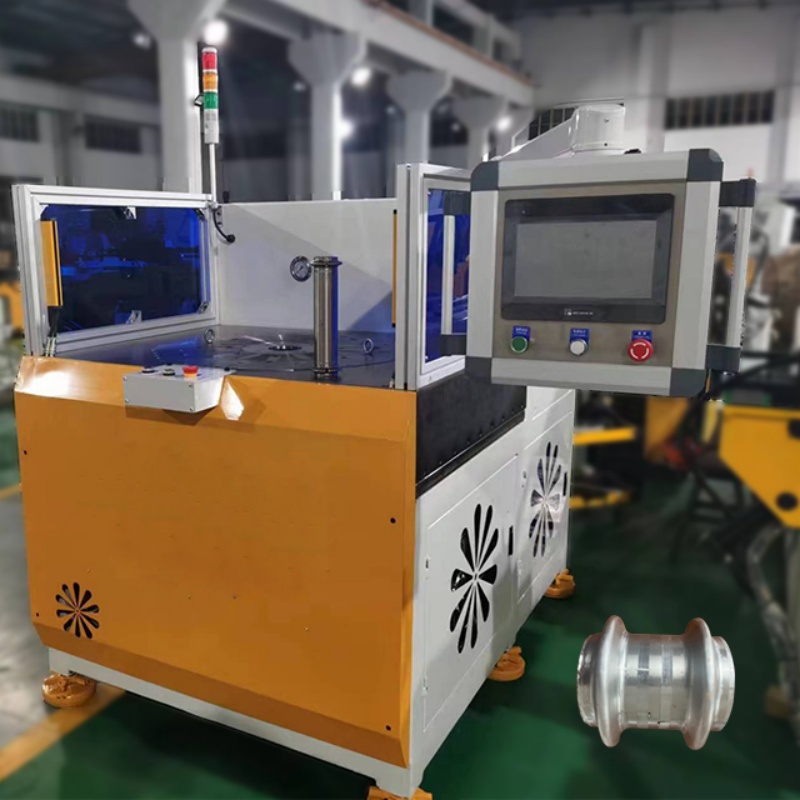
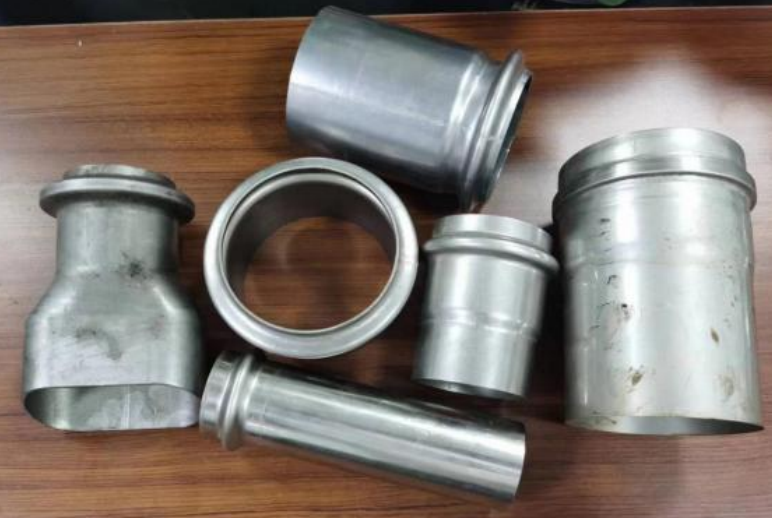
he machine is designed for forming humps, bulges and special profiles on tubes. Dedicated tooling can be configured according to the product drawing for different localized forming requirements.
The servo motor drives the hydraulic system and allows adjustment of forming speed and motion profiles. This supports smoother operation and helps control oil temperature and energy consumption during long-term production.
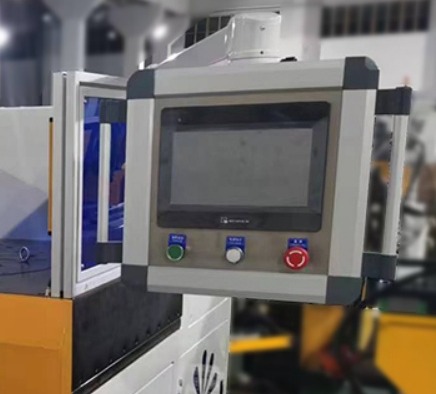
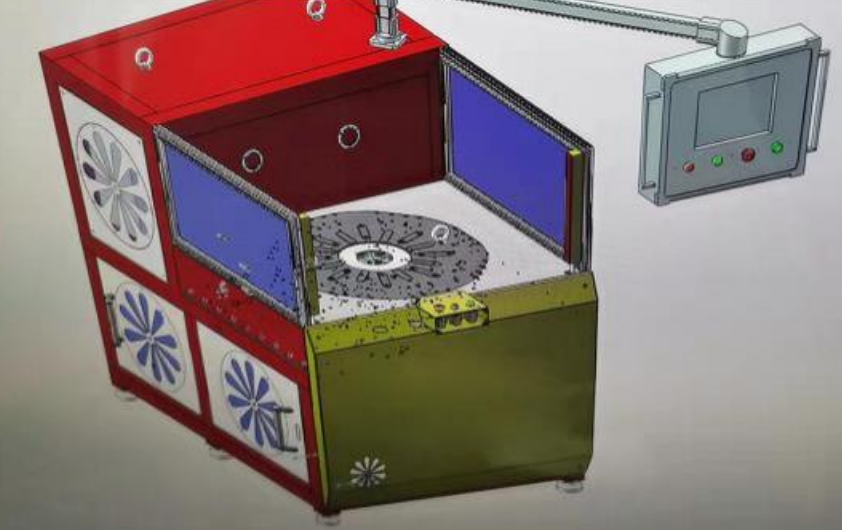
The machine uses a PLC control system and a 10-inch touch screen. Main forming data can be entered and adjusted through the HMI, making operation intuitive and product changeover convenient.
The hump diameter and contour are controlled through the coordinated operation of hydraulic cylinders, encoders and dedicated tooling. This helps improve forming position and contour consistency while reducing dimensional variation.
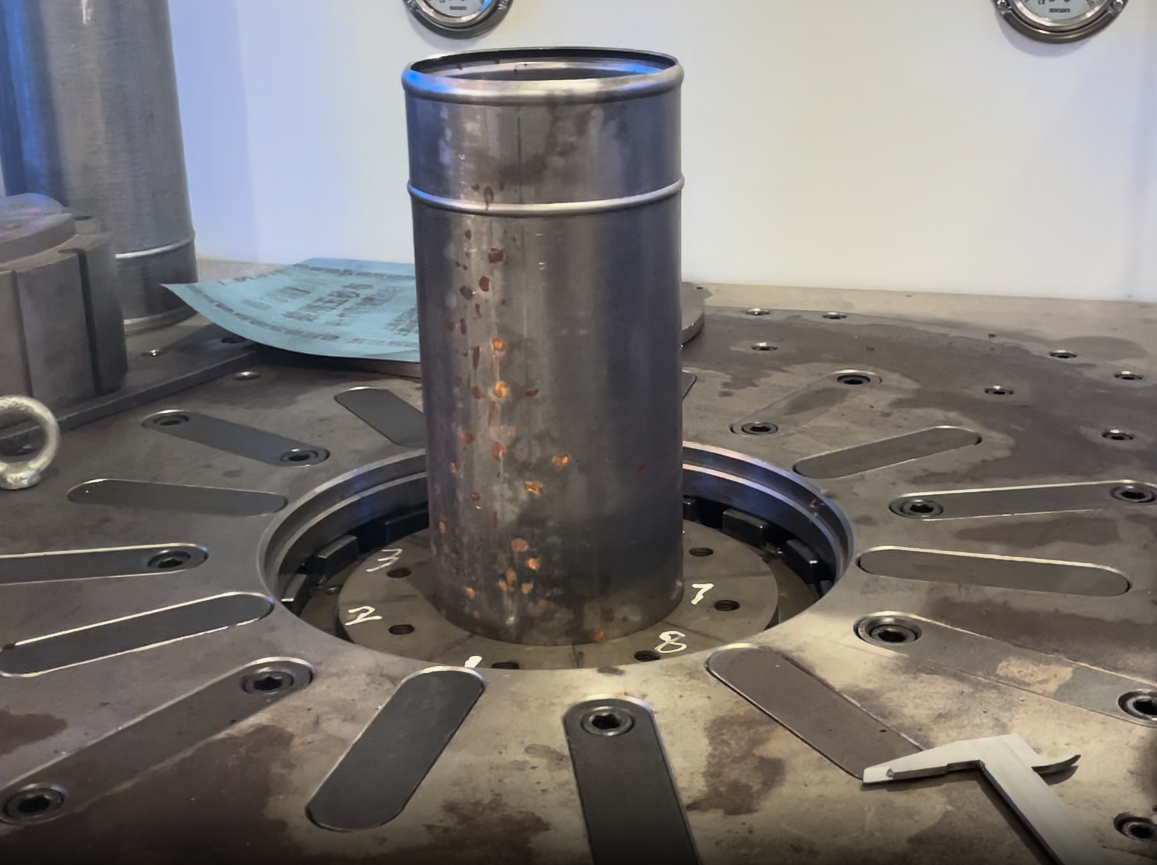
The main clamping mechanism uses a multi-point, evenly distributed layout to hold the tube securely during forming. It helps reduce slipping, displacement and local deformation.
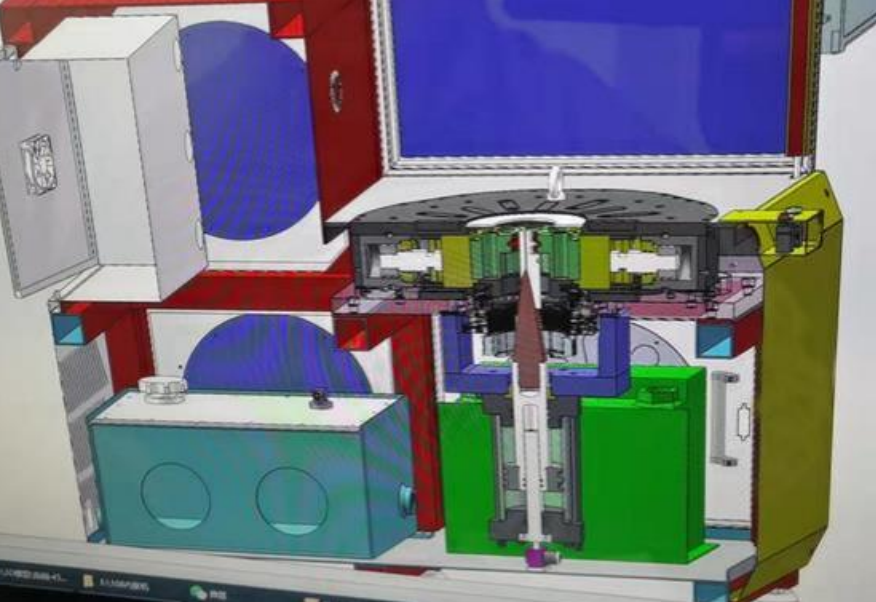
The machine is equipped with automatic lubrication, an oil cooler and an electrical cabinet cooling system. These features help maintain stable operation of the hydraulic system and key moving components during continuous production.
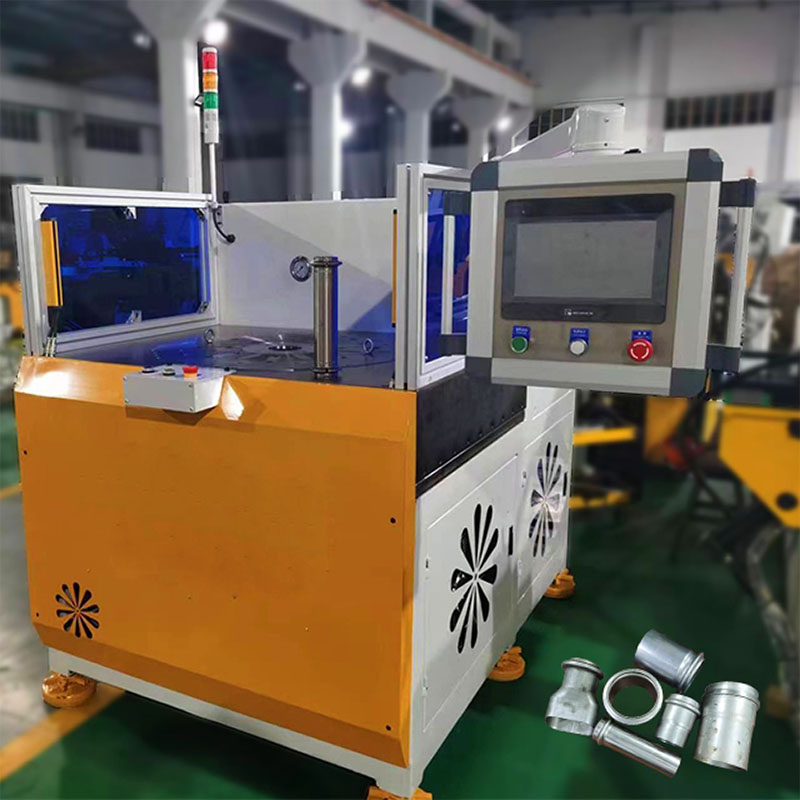
To address the challenges of inconsistent wall thickness and potential leakage risks at hose connections during the high-volume production of high-performance hump pipes for a prominent automotive exhaust system OEM supplier in Germany—where extreme forming precision is critical for secure hose fitment—Baorui Machinery deployed a high-precision pipe end forming solution; featuring superior hydraulic stability and customized mold designs, the system enables accurate extrusion forming for humps on stainless and carbon steel exhaust pipe ends. This solution ensures the hump profiles perfectly meet Germany's rigorous automotive sealing standards, significantly boosting pass rates per line while helping the client secure its core supplier status in the premium European vehicle supply chain by meeting high-frequency delivery demands.

 EN








